
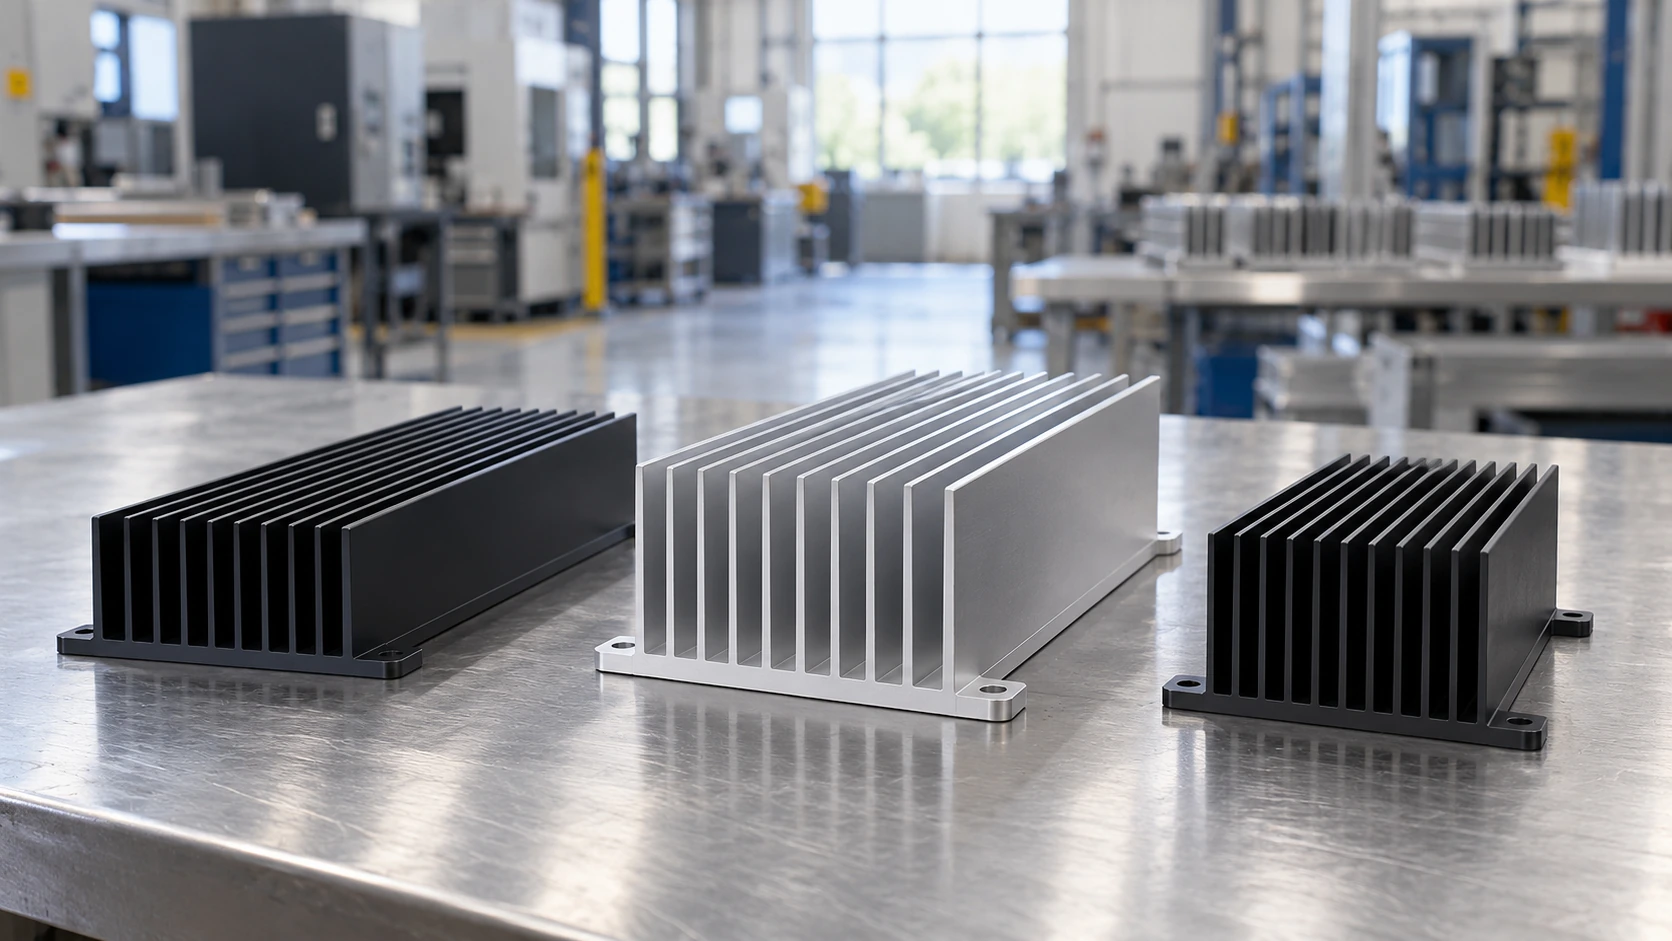
Custom Extruded Heat Sinks for Industrial Distribution
How Morton aligned three anodized aluminum profiles with one North American brand's drawings, packaging requirements and replenishment plan.
Drawing-controlled interfaces. Clear SKU identification. Stock ready for your channel.
Bring the same control to your next heat sink range.
Discuss Your Distribution Program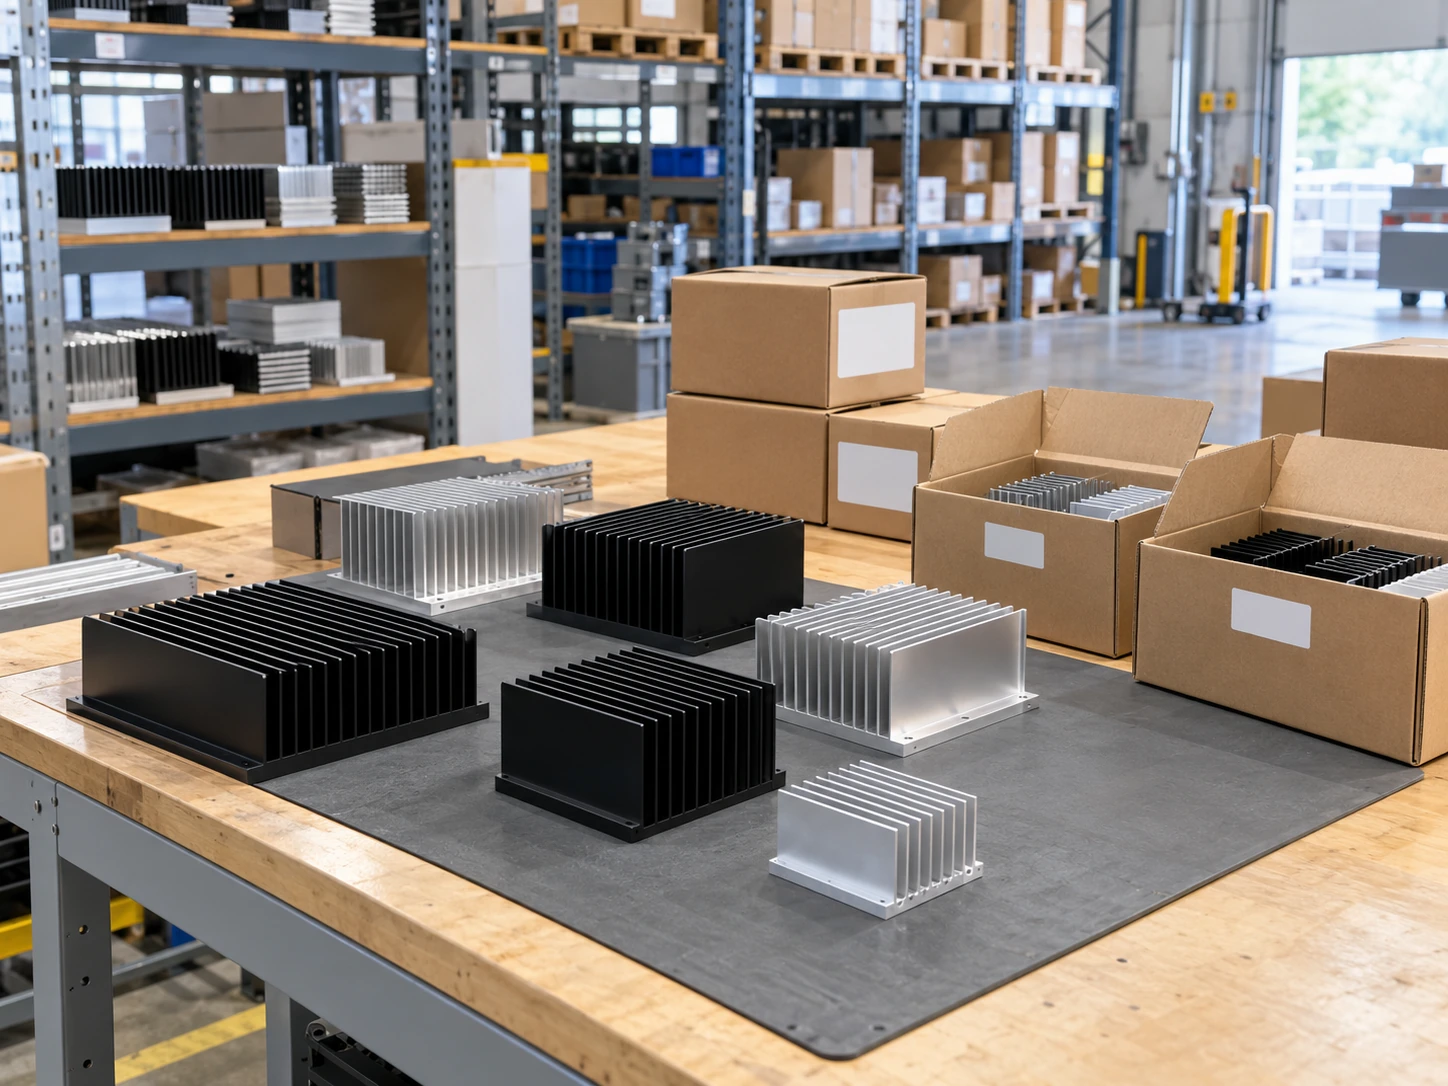
One Channel. Three Profiles. A Clear Supply Brief
A U.S. heat sink brand needed three profile variants to match existing channel products while keeping ordering and warehouse handling consistent.
Map your product range to a clear manufacturing brief.
Review Your SKU RequirementsDefine Acceptance Before Cutting Metal
The project brief converted channel risks into drawing, finish and packing requirements that engineering and purchasing could approve together.
Mounting compatibility
Control critical hole positions to ±0.05 mm against the approved datum scheme so replacement parts fit their intended assemblies.
Consistent anodized finish
Approve a finish reference for each SKU and protect specified contact, thread and grounding surfaces.
Protected fin geometry
Keep individual parts separated so fins do not carry carton compression loads or rub against neighboring parts.
Correct product identity
Match the English part number, drawing revision, barcode and carton label before shipment release.
Turn your channel's recurring issues into measurable requirements.
Set Your Acceptance CriteriaThree Profiles, Built Around Approved Interfaces
6063-T5 one-piece extrusions combine integral fins with precision secondary machining, giving each channel SKU the fit and finish its application requires.
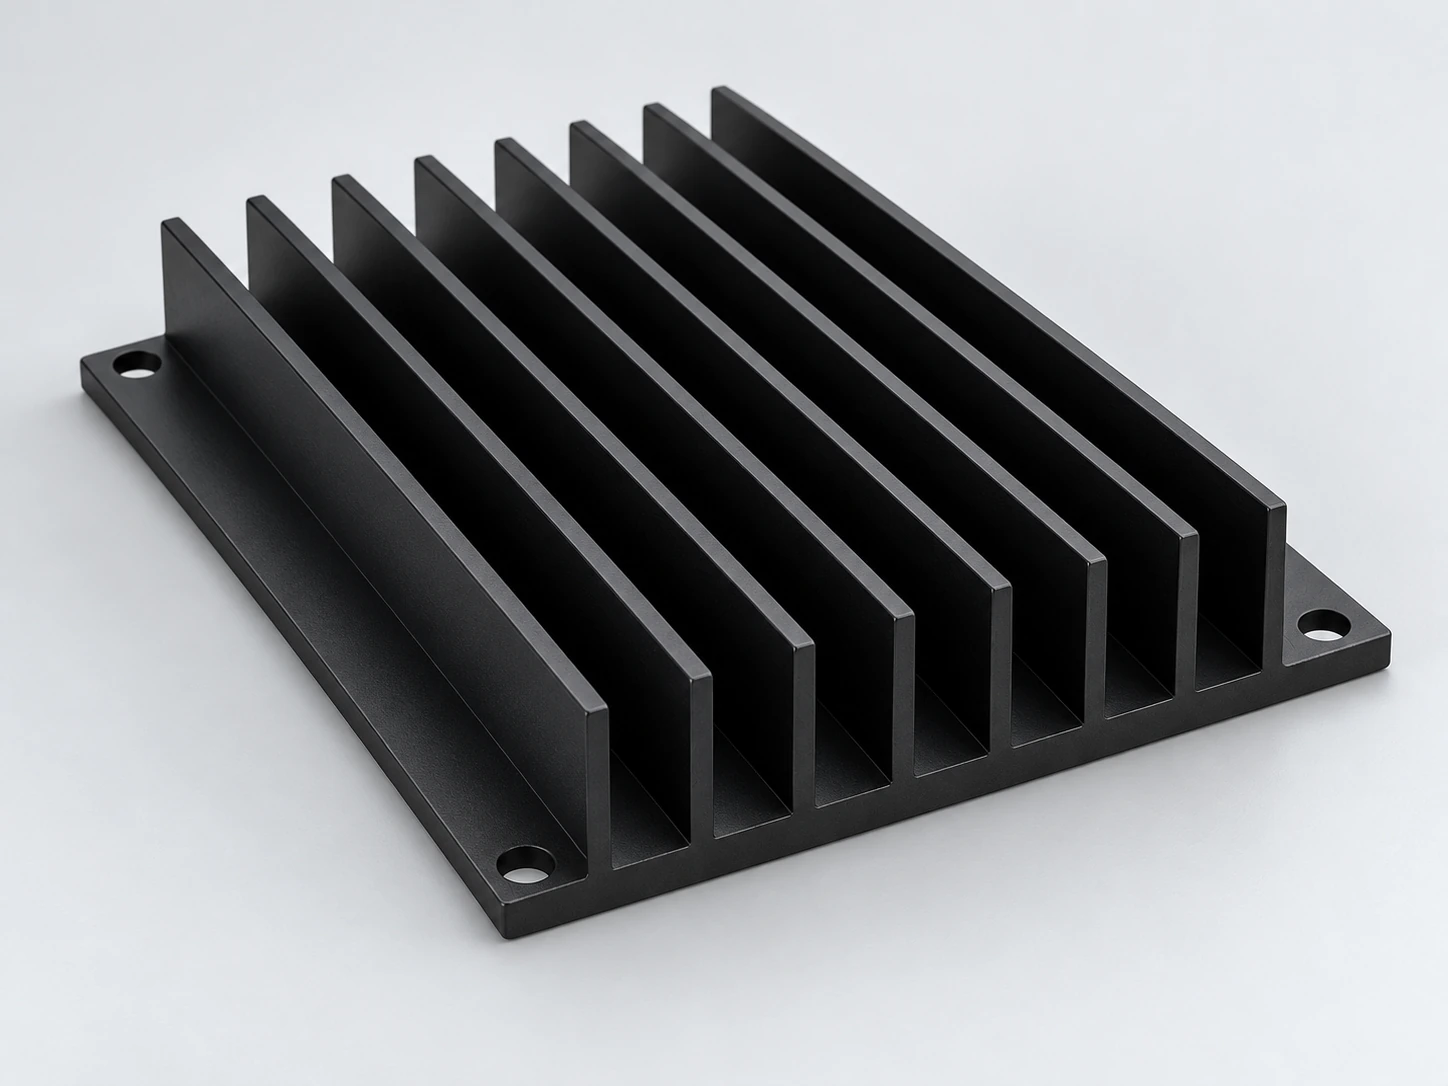
Compact Low-Profile Variant
A short fin package for space-constrained component assemblies.
- Material: 6063-T5 aluminum
- Finish: black anodized
- Interface: SKU-specific mounting pattern
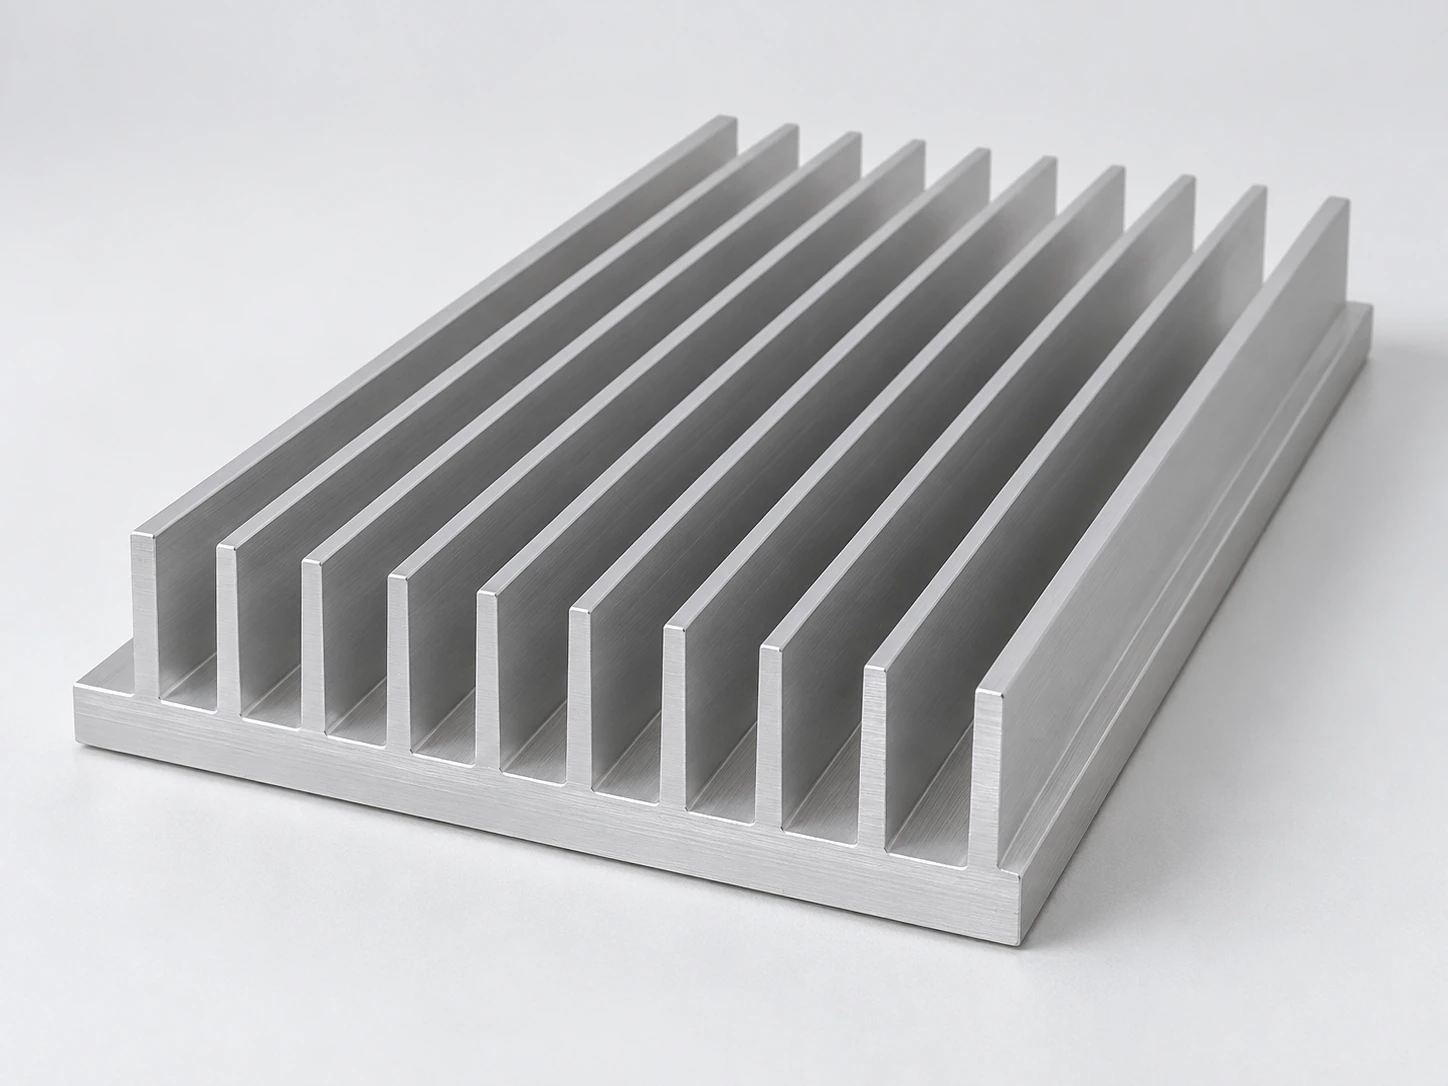
General-Purpose Channel Variant
An open parallel-fin section for common industrial component layouts.
- Material: 6063-T5 aluminum
- Finish: natural anodized
- Interface: machined thermal contact face
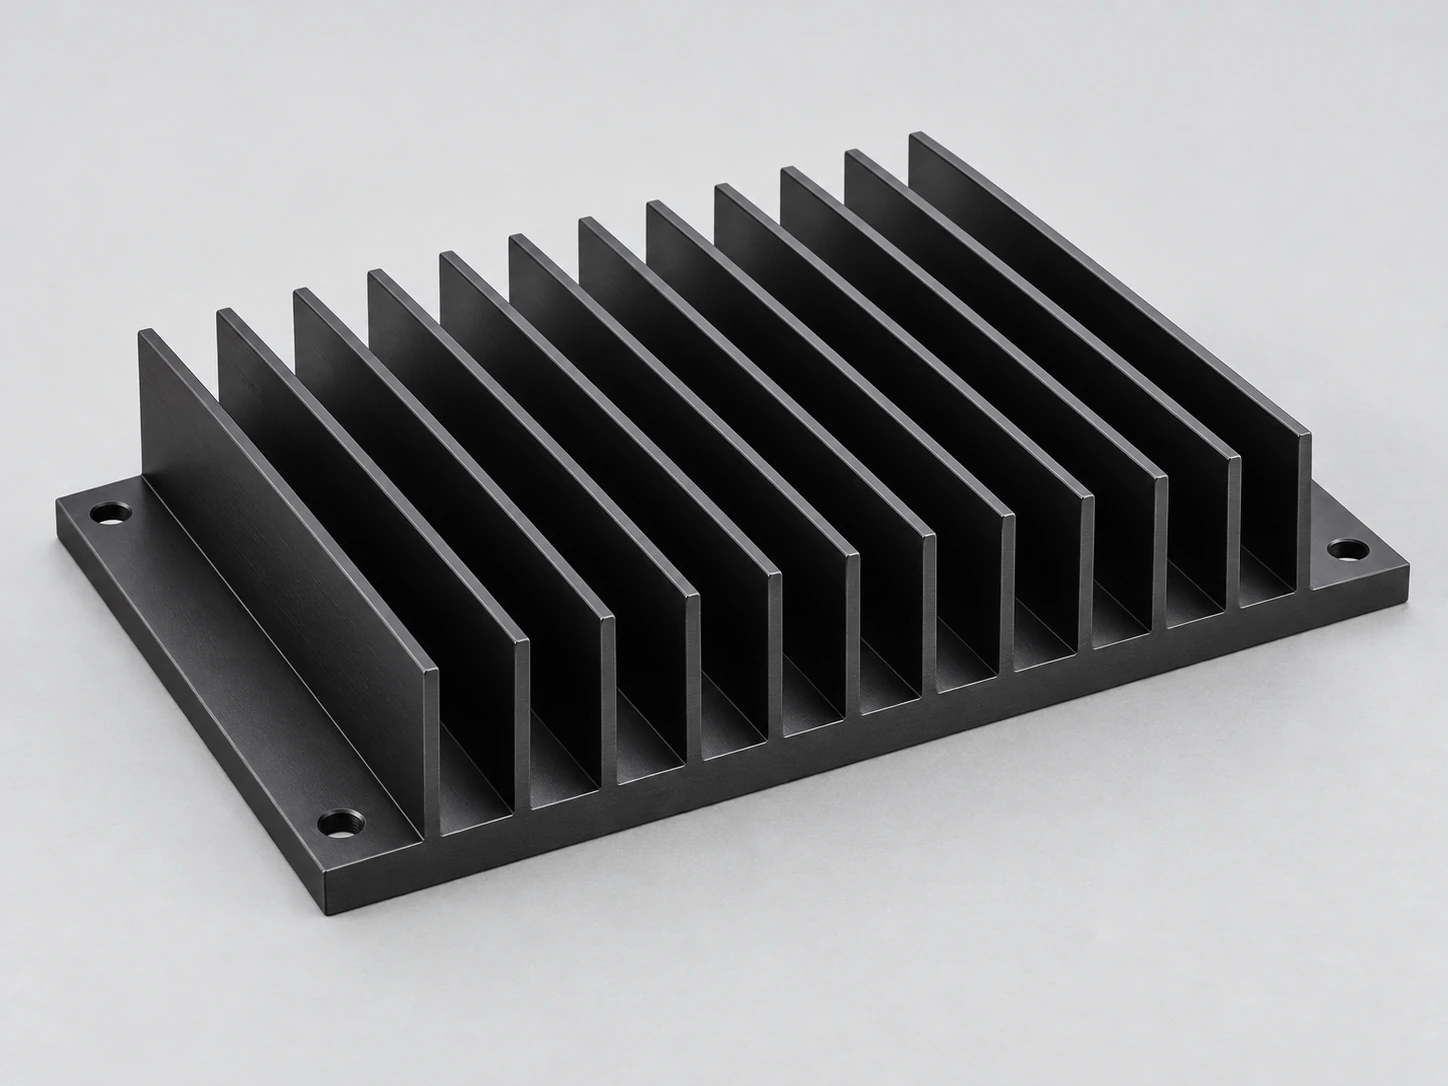
Wide-Base Power Variant
A broader mounting base for larger industrial power assemblies.
- Material: 6063-T5 aluminum
- Finish: black anodized
- Interface: drawing-controlled hole locations
Choose the profile, cut length and machining scope your channel needs.
Compare Your Profile OptionsControl the Surfaces That Decide Assembly Fit
A shared locating approach and precision-machined contact faces connect the extrusion process to the customer's final mounting requirements.
Locate from a defined datum
Use repeatable positioning fixtures and a common reference strategy for each SKU's hole pattern.
Machine the thermal interface
Finish contact faces and mounting features after cutting, then remove burrs from edges and threaded entries.
Inspect in the delivered condition
Check critical dimensions after the specified surface treatment, with masking defined on the drawing.
| Control point | Project requirement |
|---|---|
| Base material | 6063-T5 extrusion with furnace-batch identity |
| Critical hole positions | ±0.05 mm to approved drawing |
| Thermal contact face | Precision secondary machining |
| Surface treatment | SKU-specific anodized finish reference |
| Release basis | Approved revision and first-article comparison |
Resolve datums, masking and machining details before sample approval.
Discuss Your Interface DrawingPack for Resale, Trace Back to the Batch
SKU-specific dividers, barcodes and carton marks protect finished fins while preserving the link between the part and its manufacturing records.
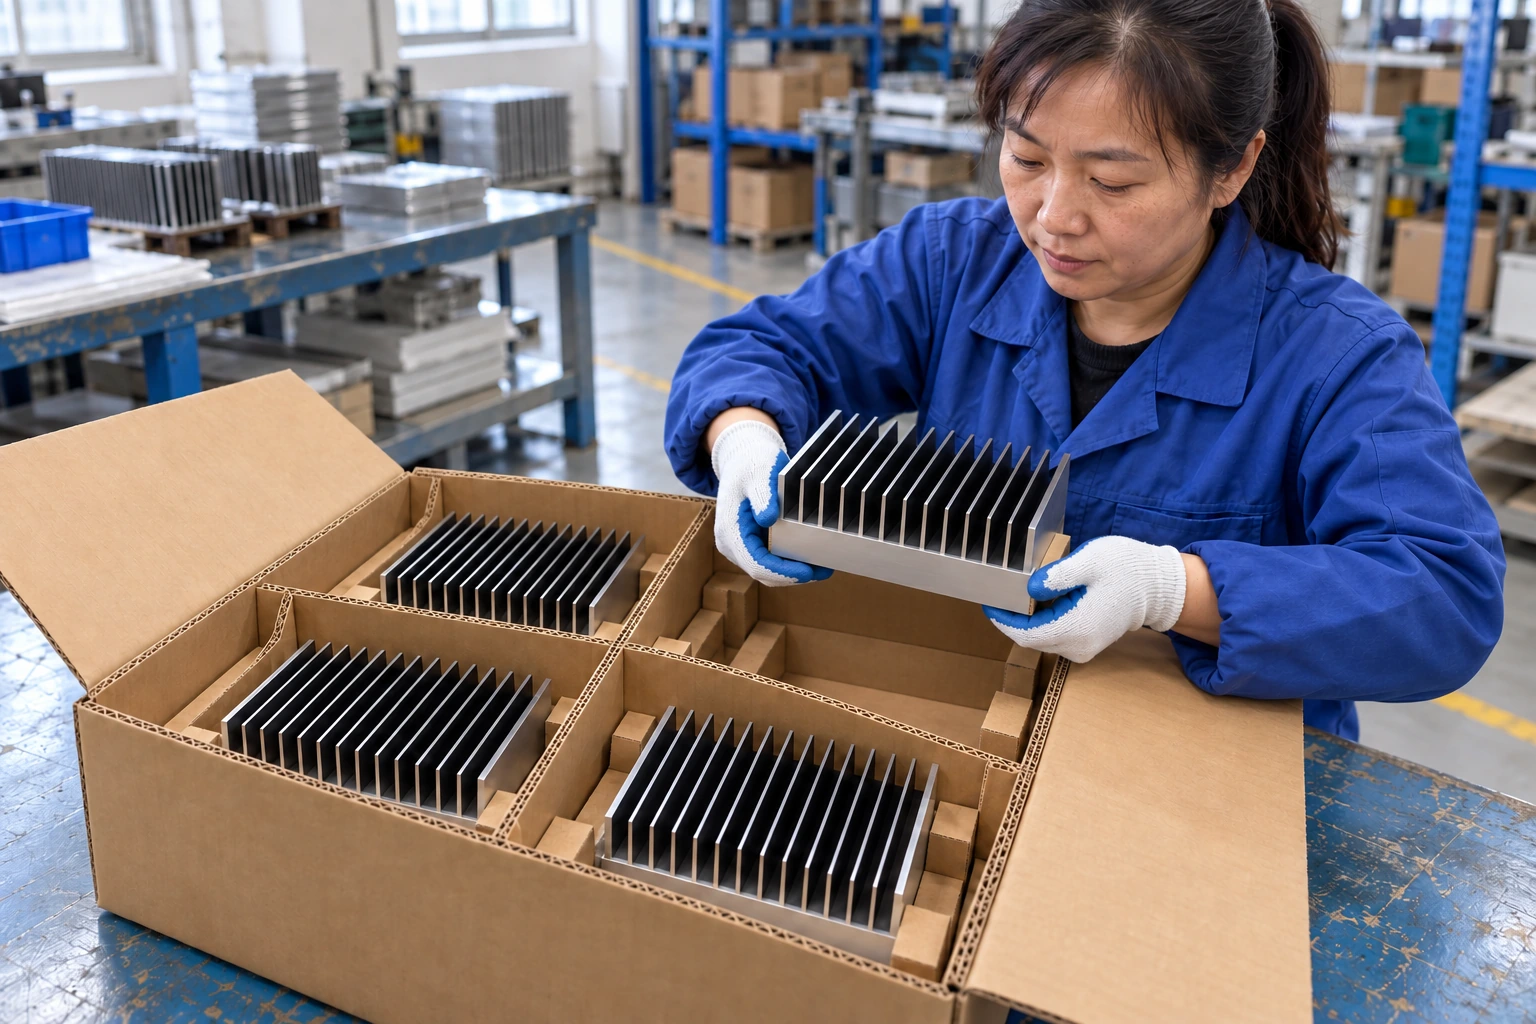
Individual protection
Separate parts with fitted dividers so anodized faces stay apart and fins remain unloaded.
SKU-specific packing
Use the approved pack quantity and English part number for each profile variant.
Readable carton identity
Align unit barcodes, carton marks and the packing list with the purchase order.
Material-to-shipment traceability
Link the extrusion furnace batch to the work order and final packaging labels.
Make your receiving and resale process part of the product specification.
Plan Your Packaging & LabelsQualification Evidence That Follows the Part
First-article approval and batch records give the distributor a practical basis for technical sign-off, incoming inspection and repeat orders.
| Approval gate | Record to review | What it establishes |
|---|---|---|
| Material identity | 6063-T5 material and furnace-batch record | The specified alloy and source batch |
| First-article fit | Assembly check for all three profiles | Compatibility with each approved interface |
| Critical dimensions | Drawing-referenced dimensional inspection | Sampled key dimensions meet the released drawing |
| Packing release | SKU, barcode and carton-mark check | Shipment identity matches the order and batch |
Controlled drawing revision
One release basis for sampling and production.
Linked manufacturing records
Material, work order and packaging remain connected.
Customer approval
First-article sign-off precedes production release.
Build a review package your engineering and receiving teams can use.
Request a Qualification ReviewFrom Approved Samples to a 3,000-Piece Release
All three first articles passed assembly checks. The first production shipment followed a defined drawing freeze, deposit and release process.
Every first-article profile passed its assembly check.
1,000 pieces per profile variant.
Measured from drawing freeze and deposit.
Sampled key dimensions conformed to the drawing.
Simpler range management
One supplier coordinated the three profile variants, their finishing requirements and packaging identities.
Clearer repeat-order control
Approved revisions, traceable batches and a replenishment plan gave purchasing a consistent reference for future releases.
Bring your target release date and annual volume into the discussion.
Plan Your First Production ReleaseQuestions Before Your Next Channel Program
Align tooling, samples, inspection and replenishment before committing a new extrusion range to your catalog.
Can you match our existing mounting interfaces?
Do we need a new extrusion die?
What sample and production quantities can we start with?
How are finish and labeling requirements approved?
How do you quote repeat orders and replenishment?
Does changing the profile change thermal performance?
Get clear answers against your drawings and commercial requirements.
Talk Through Your Program
Build Your Next Heat Sink Range with Morton
Share your profile drawings, target quantities and packaging requirements. We will help define a practical route from sample approval to repeat supply.
Tell us which profiles you need and how your channel receives them.